Moulds Presses Tools Cleaning


Professional Mould Press And Tool Cleaning Services Australia
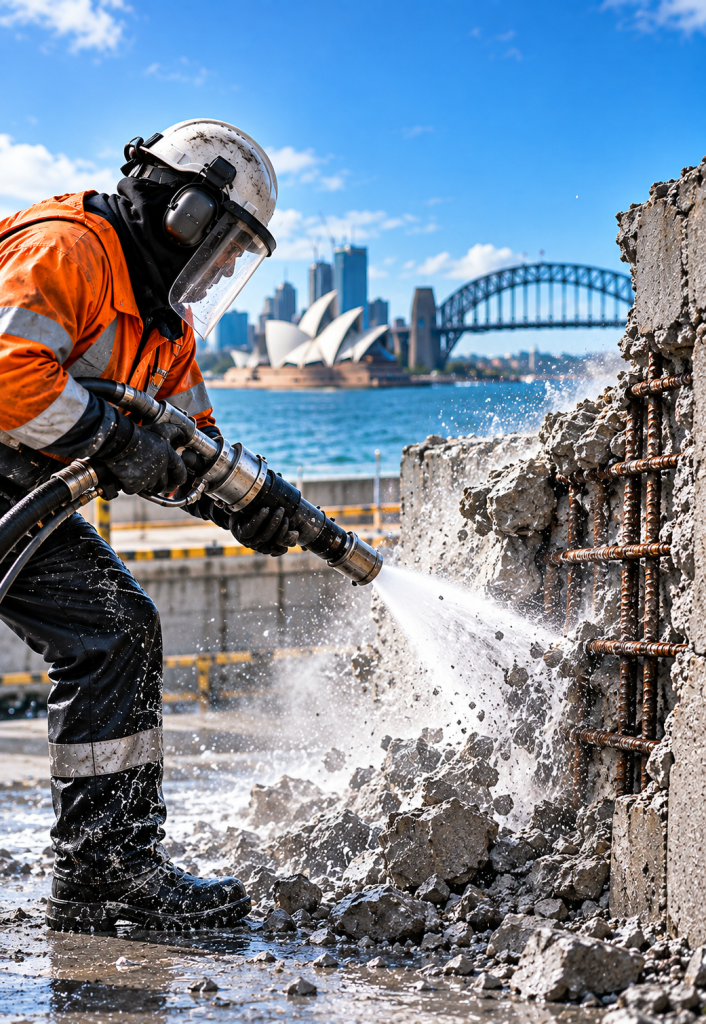
When reject rates creep up and nobody can point at the cause, your tooling is usually carrying the answer in its cavities. Mould cleaning services from H2O Quantum Tech remove resin, carbon, release agent and scale from moulds, dies and press tooling without touching the surface finish underneath. Our press cleaning services cover platens, bolsters, tie bars and frames, so the whole machine comes back clean rather than just the tool face. Injection mould cleaning is done with water pressure alone, so no abrasive, bead or chemical residue is left sitting in the vents. Production teams searching tool cleaning near me reach crews used to working inside tight changeover windows, on site, without sending expensive tooling away for a week.
The Reject Rate Nobody Traces Back To Tooling
Contamination changes parts long before it changes anything you can see on a gauge. A film left where release agent removal was skipped alters surface finish and hides fine detail in the cavity. Carbon and resin buildup removal in vents stop gas escaping, and short shots, burn marks and dimensional drift follow within a shift. On press tooling, scale between the die and the bolster changes shank height and loads the frame unevenly. Die cleaning services deferred long enough allow gas burn into the steel itself, and that damage is permanent. Cycle times stretch as operators compensate on parameters, scrap climbs quietly, and your tool room ends up polishing tools that only ever needed cleaning, which shortens the working life of every tool it touches.
Why Manual Polishing Slowly Destroys Expensive Mould Surfaces
Every abrasive pass takes metal you never get back. Stones and emery cloth round sharp edges, soften textures and open tolerances that were expensive to cut in the first place. Bead blasting embeds media in vents and cooling channels, and it changes surface roughness right across the cavity. Chemical strippers attack the steel around inserts and leave residue that flashes off into your first parts. Ultrasonic tanks work, but a large tool waits days for its turn and comes back wet in every water line. Precision tooling cleaning with controlled water pressure removes only the deposit, and extrusion die cleaning reaches land surfaces and bearing areas that nothing else touches, including channels too fine for any mechanical tool.
Precision Water Cleaning That Preserves Cavity Detail Exactly
Each tool is assessed first, so alloy, surface finish, texture and insert construction set the pressure we work at. Industrial mould cleaning Australia wide then proceeds with graduated pressure, starting conservative and increasing only until the deposit releases. Vents, gates, cooling channels and press platen cleaning areas are all addressed in the same visit, then the tool is dried, corrosion protected and left ready to run. Where the tool stays in the machine, tool cleaning Perth and Sydney crews contain the work area and protect platens, slideways and guarding throughout. Photographic before and after records go back with the tool, so your tool room holds evidence of the condition it was returned in. Over a few cycles that record shows you which tools foul fastest and why, which is information worth having before the next campaign.
What Your Tool Room Gets Back From Us
- Cavity detail, texture and tolerances survive the cleaning intact
- Vents and gates flow again so gas burn stops
- Reject rates fall because surface finish returns to specification
- No abrasive media is left in cooling channels or vents
- Cycle times recover without operators compensating on machine parameters
- Tools come back dried and corrosion protected, ready to run
- Presses, platens and bolsters are cleaned in the same visit
- Before and after records supplied for your tool history file
- Work fits inside planned changeover and maintenance windows
Can You Clean Moulds Without Removing Surface Texture
Yes. Pressure is set against the texture and finish of your specific tool and only the deposit is removed. Nothing abrasive contacts the cavity, so etched and grained surfaces stay intact.
How Long Are Our Presses Out Of Service
Most in machine tool cleaning is completed within a single shift. Larger tools and full platen cleaning can need longer, and we confirm the duration in writing before mobilising to your site.
Do You Clean Tooling On Site Or Offsite
Both. We clean in the machine or in your tool room where access allows, and can collect larger tooling for cleaning and return where a longer window is available.
Is This Suitable For Food Grade Production Tooling
Yes. Water only cleaning suits food and pharmaceutical tooling because no solvent, detergent or abrasive residue remains behind. The work is documented so your quality team can close out verification.